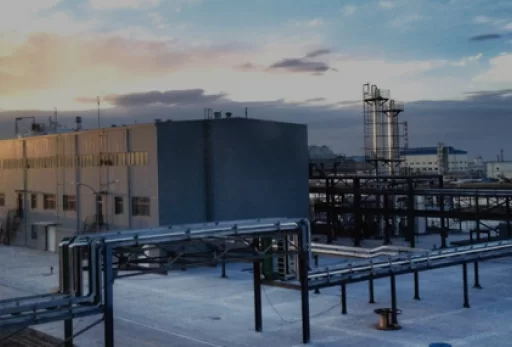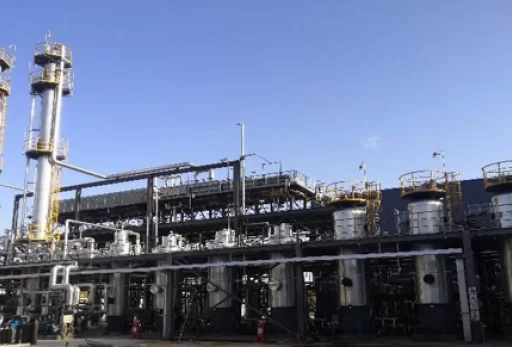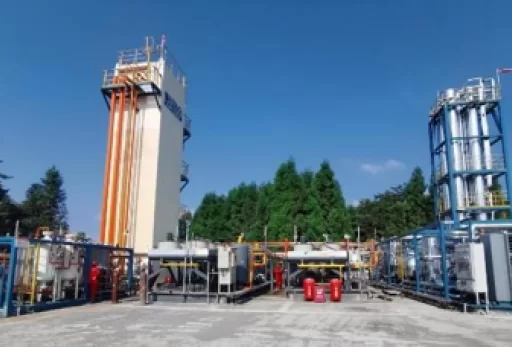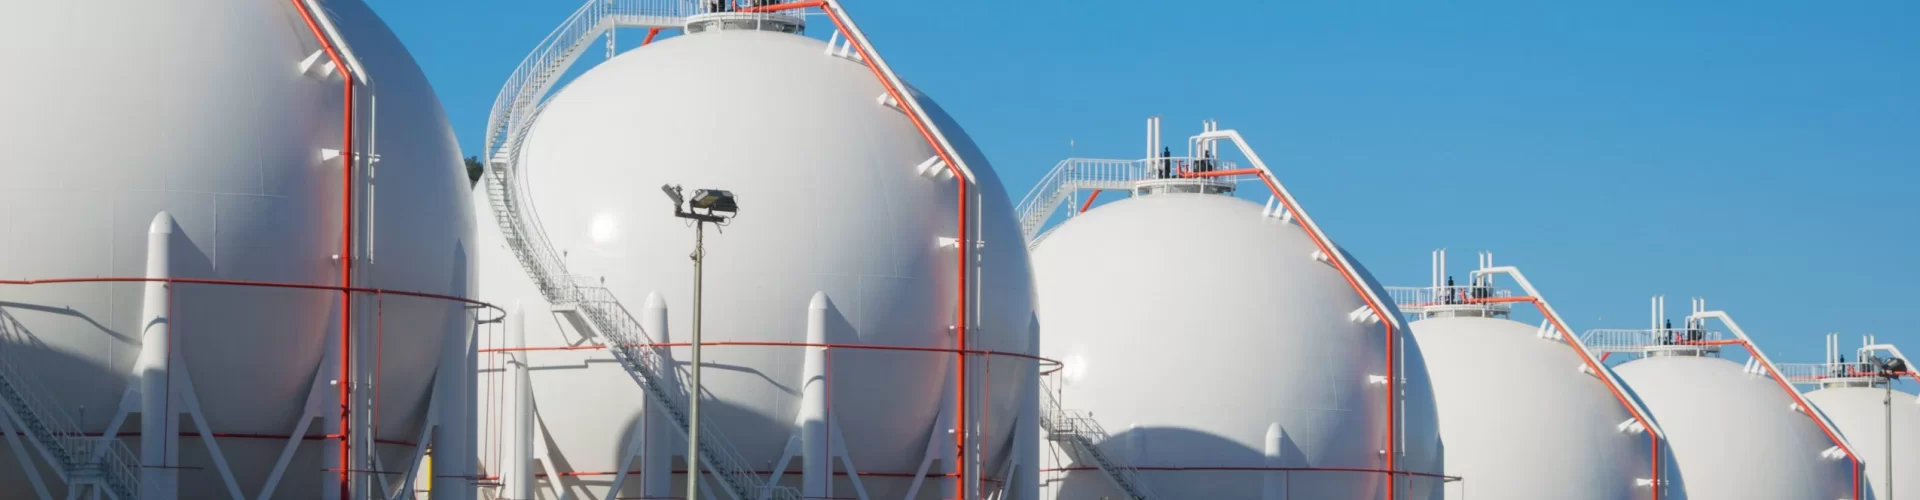
Our advanced Natural Gas Liquefaction (LNG) and Treatment solutions provide a comprehensive end-to-end approach to transforming raw feed gas into high-value liquid energy. By integrating cutting-edge purification and cryogenic technologies, we ensure that your gas stream is stripped of impurities and liquefied with maximum energy efficiency, adhering to the most stringent international quality standards.
Designed for versatility, our systems support a wide array of feedstocks, including pipeline and associated gases. Whether you are deploying a massive onshore plant or a flexible floating LNG (FLNG) facility, our modular and customized engineering ensures seamless integration, operational safety, and optimized throughput for global energy distribution.
| Processing Capacity | 100,000 – 5 Million Nm³/day | Liquefaction Efficiency | > 85% |
|---|---|---|---|
| Pretreatment Scope | Dehydration, Deacidification, Demercuration | Impurity Level | Reduced to ppm level |
| Storage Temperature | -162°C (Adiabatic) | Cold Loss Rate | < 0.15% |
| Supported Feedstocks | Pipeline Gas, Associated Gas | Deployment Scenarios | Onshore Plants, Floating FLNG |
| Compliance | International Gas Quality Standards | Recovery System | Integrated BOG (Boil-Off Gas) Recovery |
Integrated purification removes water, acids, and mercury to ppm levels, protecting downstream equipment from corrosion.
Achieving liquefaction efficiency over 85%, significantly reducing the energy cost per unit of LNG produced.
Flexible capacities ranging from 100k to 5M Nm³/day to match your specific resource scale and market demand.
Specialized engineering for floating platforms, enabling gas monetization in remote offshore locations.
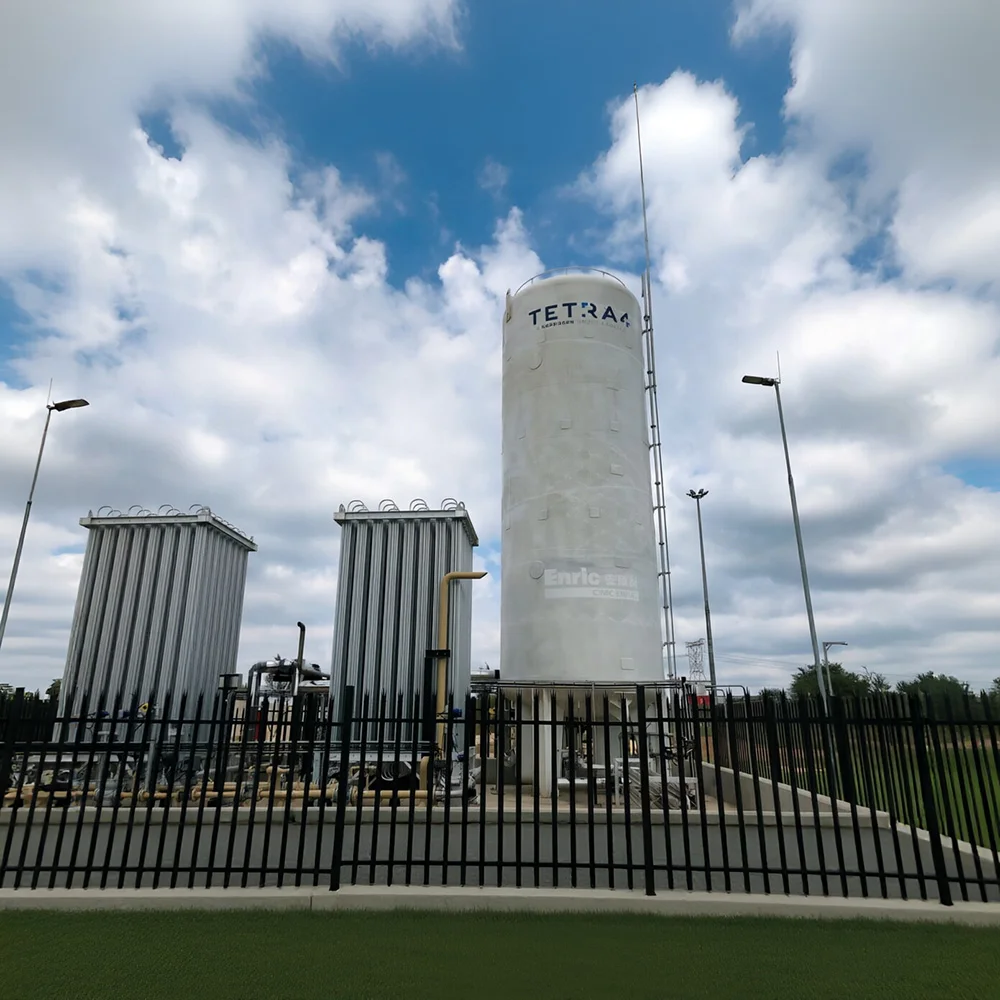
Adiabatic storage tanks maintain -162°C with a loss rate below 0.15%, ensuring maximum product retention.
Integrated Boil-Off Gas recovery minimizes waste and enhances the overall economic viability of storage.
Real-time monitoring of pipeline and associated gas composition for precise treatment adjustment.
Fully automated control of the liquefaction cycle to maintain efficiency above 85% consistently.
Instant notifications when pretreatment levels deviate from international ppm quality standards.
Continuous tracking of adiabatic tank temperatures to prevent unplanned boil-off events.
Precise measurement of LNG volume and BOG recovery rates for optimized logistics planning.
Analytics dashboard to track and reduce power consumption during the cooling process.
| Metric | Standard Systems | Our Advanced Solution |
|---|---|---|
| Energy Efficiency | 70% - 80% | > 85% |
| Cold Loss Rate | 0.3% - 0.5% | < 0.15% |
| Impurity Control | General Grade | ppm Level / Int'l Std |
| Deployment Flexibility | Fixed Onshore Only | Onshore & FLNG |
| OpEx (Energy Cost) | Baseline | Reduced by 15-20% |
Our units are highly adaptable and can process various feedstocks, including pipeline natural gas and associated gas from oil production, ensuring versatility across different extraction sites.
We use an integrated purification system that performs dehydration, deacidification, and demercuration, reducing impurities to the ppm level to comply with international gas quality standards.
The Boil-Off Gas (BOG) recovery system captures gas that naturally evaporates during storage, re-liquefying it or using it as fuel, which significantly reduces product loss and operational costs.
Yes, our customized liquefaction units are specifically engineered to support both onshore plants and floating LNG (FLNG) scenarios, providing flexibility for offshore resource development.
We offer a wide range of capacities to suit different project scales, typically ranging from 100,000 to 5 million Nm³ per day.
By utilizing -162°C adiabatic storage tanks combined with advanced insulation and our BOG recovery system, we keep the cold loss rate below 0.15%.